Technical article
How Servo Technology Exceeds Highest Demands
Small impurities, big disaster. In the production of pharmaceutical primary packaging or medical plastic parts such as highly precise Luer-Lock systems, cleanliness for the machine, tool, and moulded part is not just a formality, but a strictly regulated production standard, compliance with which determines the success or failure of entire batches. No one wants to have thousands of parts produced in vain - because of contamination on the screw cap. Servo-electric automation concepts not only perform translational and linear movements reliably, but also minimize contamination risks. But what technology is exactly behind this? Let's take a closer look at the servo advantages under the microscope.
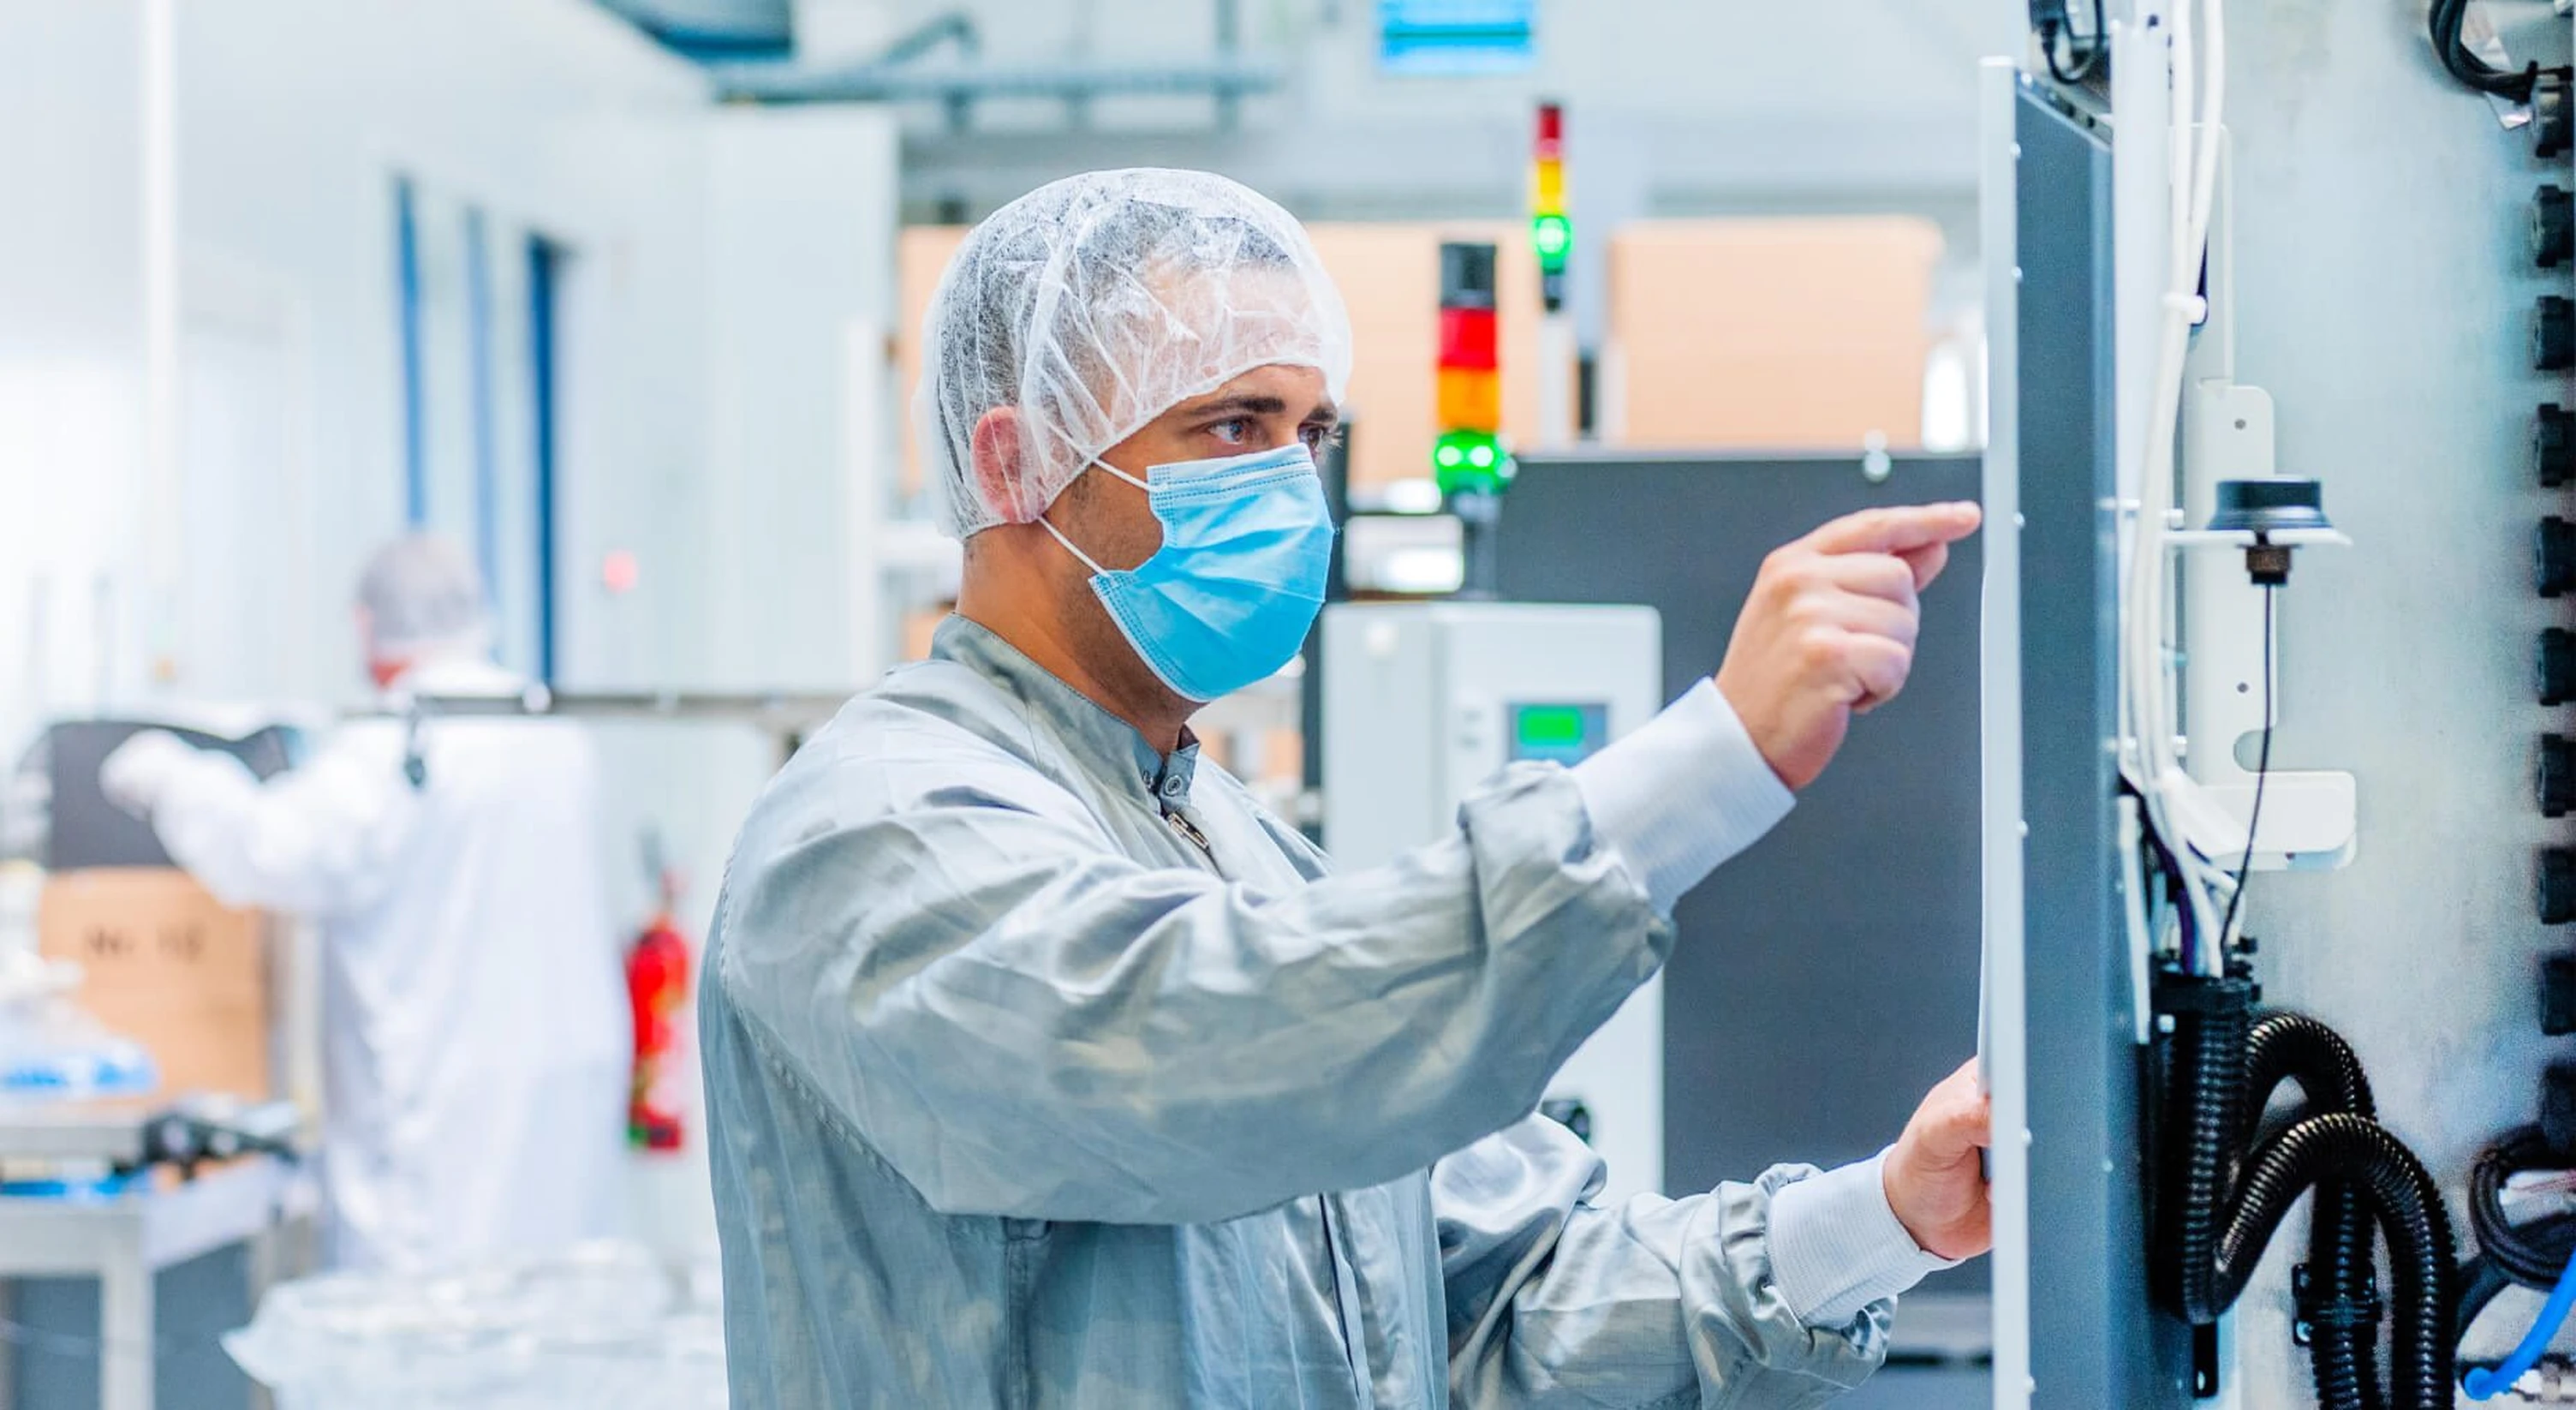
Cleanroom injection moulding places special requirements on the mould and drive technology
Servo-electric mould drives are designed for cleanroom use and are typically deployed in environments up to ISO 7 in accordance with ISO 14644-1 – equivalent to EU GMP Grade C (at rest) or Class 10,000 under the former FED-STD-209E. They operate without hydraulic oil, with minimal waste heat and low particle emission.
Where maximum cleanliness counts, no oil may enter the process. Injection moulds and moulding machines with hydraulic drives therefore reach their limits in the cleanroom: only with considerable extra effort – such as enclosing the hydraulic blocks or using special FDA- or NSF-compliant lubricants and hydraulic oils – can the contamination risks be reduced.
For injection moulding machines in cleanroom applications, the trend has clearly been moving towards all-electric machines for years. Within the injection mould itself, hydraulic drives can also be replaced entirely by servo-electric system solutions: the servo motors used are brushless and fanless, clean and energy-efficient. They require no hydraulic oil; the remaining lubrication of guides and gears is encapsulated and reduced to a minimum.
Cleanroom classes in injection moulding: ISO 14644-1 (ISO 7/8) and GMP
Cleanrooms are classified according to ISO 14644-1 based on the maximum permissible particle concentration per cubic metre of air – from ISO 1 (the cleanest class) to ISO 9. In injection moulding for medical technology and diagnostics, production predominantly takes place in ISO 7 or ISO 8; the very clean classes ISO 1 to ISO 5 remain reserved, as far as injection moulding is concerned, for special cases such as semiconductor manufacturing.
For pharmaceutical applications, the EU-GMP guideline (Annex 1) with its classes A to D also applies. The older US standard FED-STD-209E was withdrawn in 2001, but its designations – such as “Class 10,000” – are still in common use in practice. The classes can be mapped approximately as follows:
ISO 5: max. 3,520 particles ≥ 0.5 µm/m³ · EU GMP Grade A/B · formerly Class 100
ISO 6: max. 35,200 particles ≥ 0.5 µm/m³ · formerly Class 1,000
ISO 7: max. 352,000 particles ≥ 0.5 µm/m³ · EU GMP Grade C · formerly Class 10,000
ISO 8: max. 3,520,000 particles ≥ 0.5 µm/m³ · EU GMP Grade D · formerly Class 100,000
Note: GMP classes are assessed at rest and in operation – Grade C corresponds to approximately ISO 7 at rest and approximately ISO 8 in operation.
Which class a project must meet depends on the product and the regulatory environment – typical use cases are shown in the overview of injection moulding solutions for medical technology and pharma. What matters from the drive technology perspective: it must not introduce any additional contamination source such as hydraulic oil into the cleanroom.
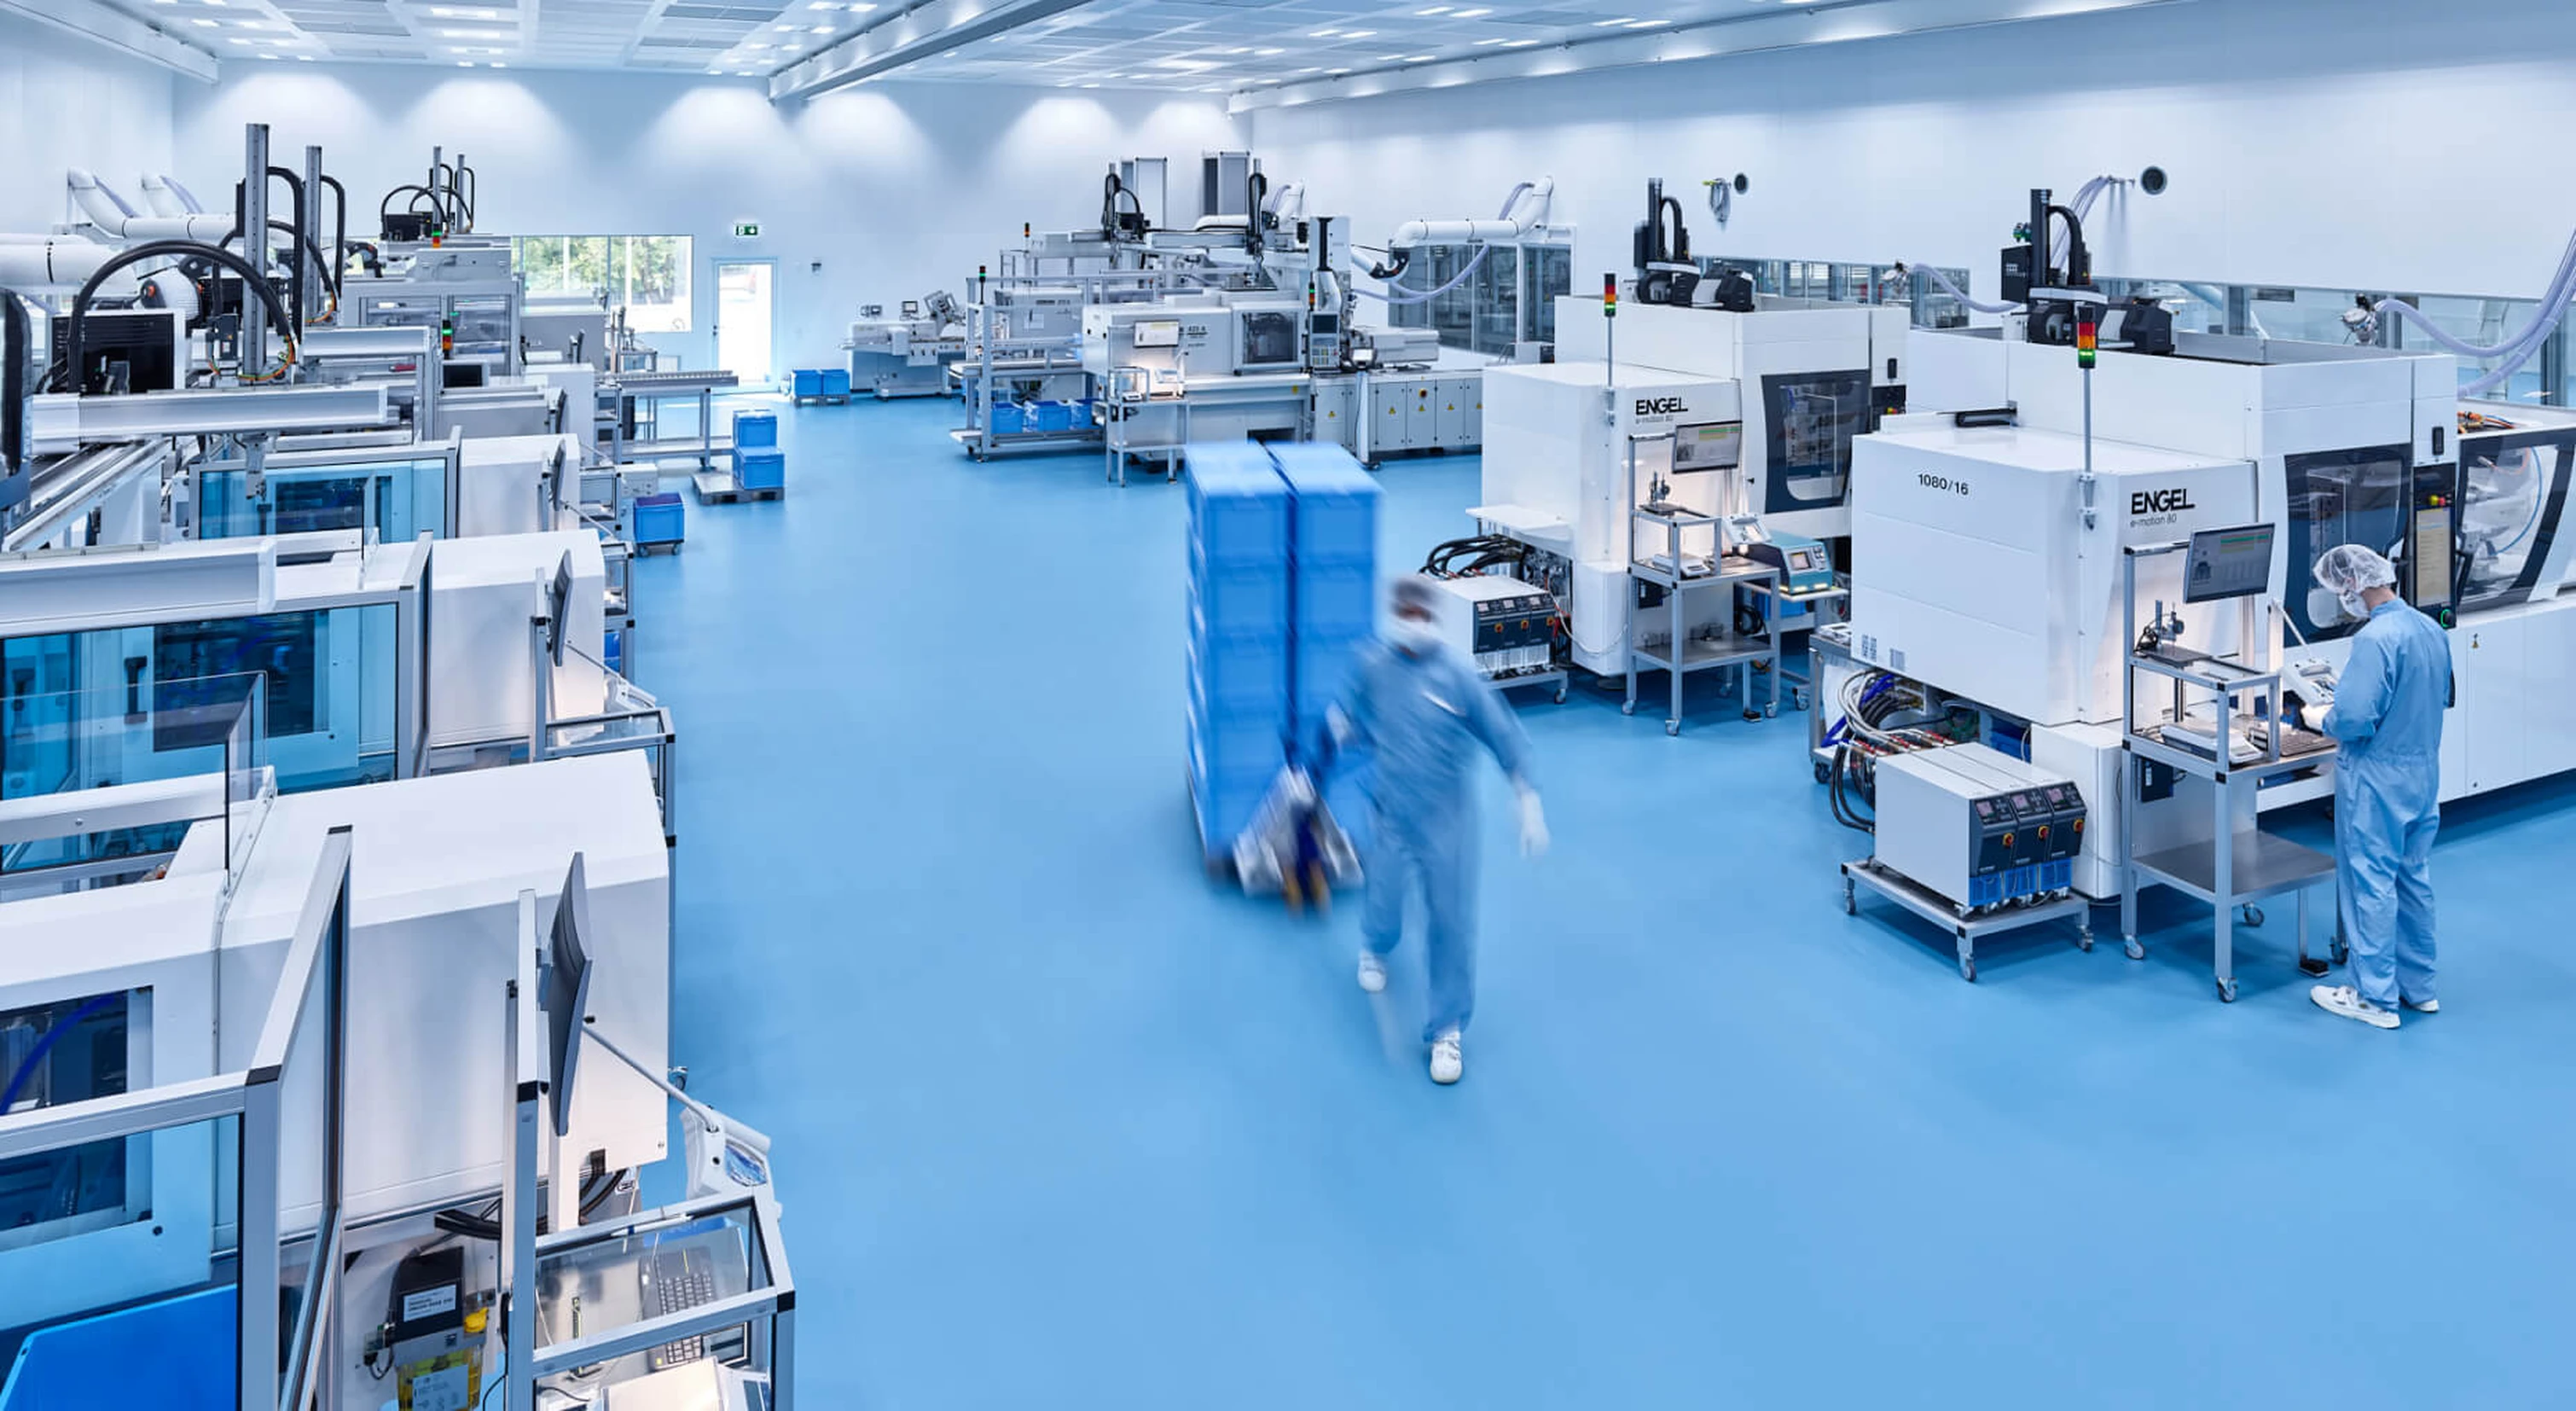
The company Wild & Küpfer relies on Servomold for cleanroom production.
Requirements for the injection mould in the cleanroom
In addition to the environmental class, the cleanroom places specific requirements on the design and construction of the injection mould itself:
Corrosion-resistant tool steels: Frequent cleaning and disinfection cycles as well as controlled, sometimes humid conditions require rust-resistant steel grades; martensitic tool steels (e.g. 1.2083) are common for cavity-forming components.
Flash-freedom and tight gap dimensions: Parting lines, slides and ejectors must be manufactured to the tightest tolerances so that no flash occurs – critical for components in contact with blood or medication, such as Luer-lock connectors.
Surfaces and coatings: Smooth, polished surfaces without dirt traps make cleaning easier. Wear-resistant PVD coatings (e.g. chromium nitride or DLC) reduce abrasion on moving components.
Encapsulated mechanics and minimised lubrication: Moving assemblies are designed to be encapsulated; where lubrication is unavoidable, food-grade lubricants (NSF-H1-registered) are used in minimised quantities.
Drive technology without hydraulic oil: Core pulls, unscrewing movements and slides can be driven servo-electrically instead of hydraulically – eliminating the largest potential contamination source in the mould.
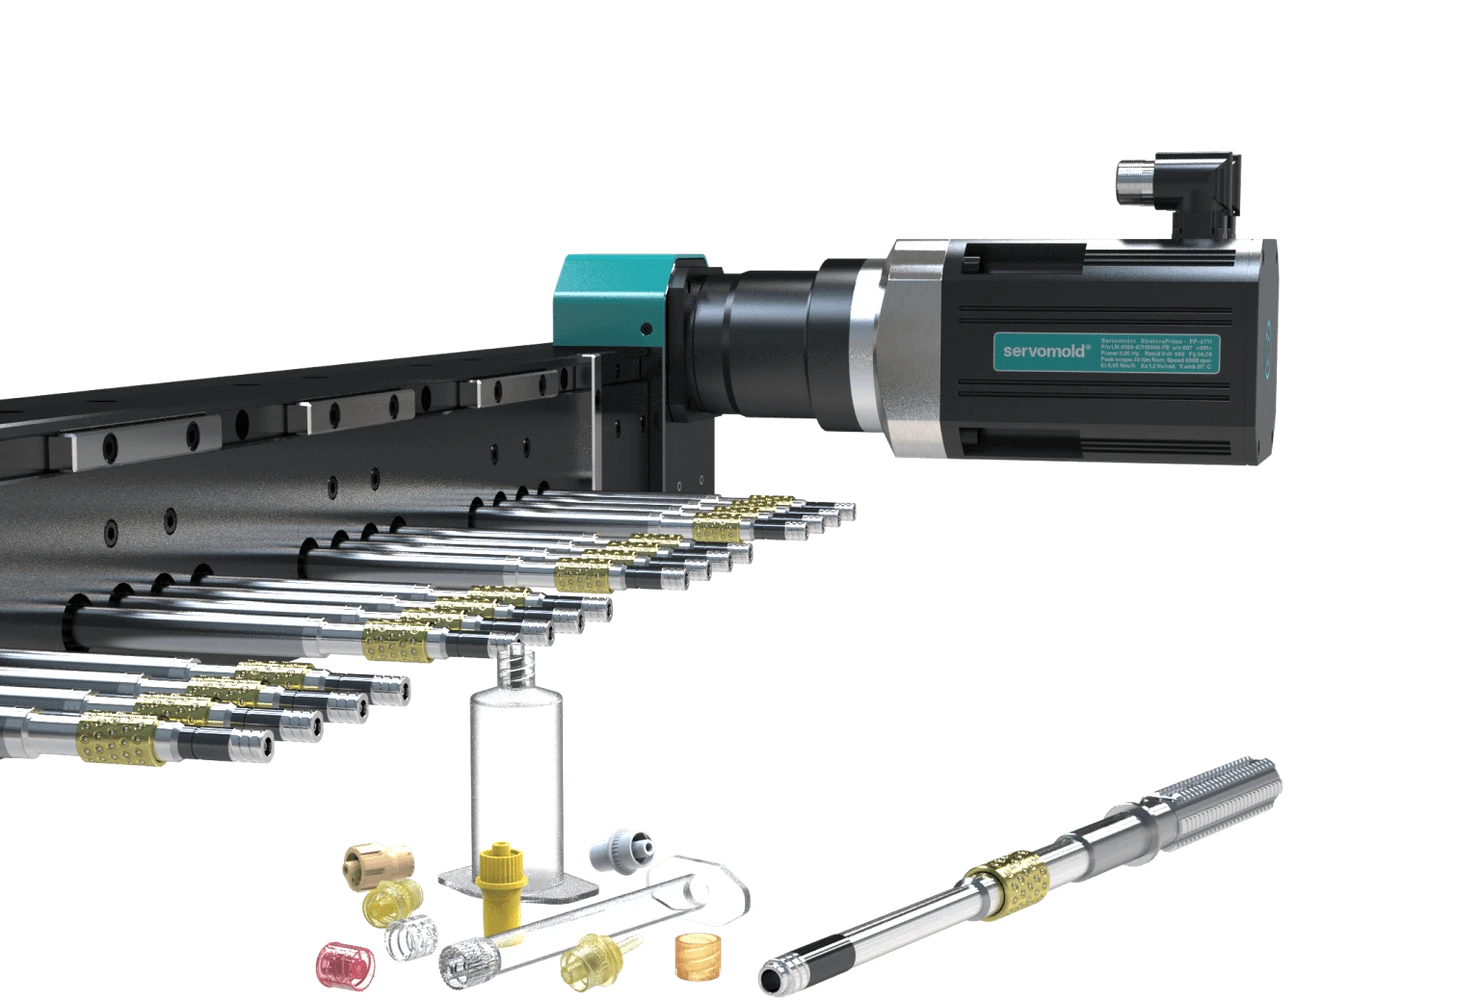
Precise, repeatable mould movements ensure flash-freedom and tight tolerances
Alongside freedom from contamination, outstanding precision and manufacturing quality are among the key characteristics of cleanroom production. The basis for this is provided by systems that allow manufacturing processes and mould movements to be set up and repeated with a high level of detail.
An important aspect is the required flash-freedom of plastic parts that will later come into contact with blood – injection moulds for Luer-lock systems, for example, must be manufactured with very tight tolerances and the narrowest gap dimensions. Combined with the required reduction of lubricants and highly dynamic movements for short cycle times, this creates a situation that is difficult to control with hydraulic systems and their limited adjustability.
Servo drives can be controlled sensitively and with pinpoint accuracy thanks to the position encoder fitted to the servo motor – such as an electromagnetic resolver or optoelectronic absolute encoders. Depending on the system, one revolution of the motor shaft is resolved into hundreds to thousands of increments, with which the servo controller guides the motor to within a few arc minutes. This enables micron-accurate positioning of mechanisms without using a hard end stop. Torque, forces and speeds can be limited and permanently monitored – this reduces mechanical loads and extends the service life of the injection mould.
Verifiable quality and stable processes
Without a corresponding servo controller, a servo motor will not move a single millimetre – this prerequisite is at the same time the greatest strength of servo technology.
Modern servo controllers not only provide full control of the movements, they also enable the acquisition of relevant process parameters and thus contribute to the continuous monitoring of product quality.
Process monitoring via torque and motor temperature
Analysing the torque and temperature of the servo motor allows direct conclusions to be drawn about the consistency of movement sequences and provides important indications in the event of process deviations. Changes or wear on the injection mould can be detected early and rectified in a targeted manner.
Material- or parameter-related changes to the injection moulding process also become visible – different injection pressures, for example, are reflected in changes to the demoulding forces. In this way, the process monitoring of the servo controller ensures stable and verifiable processes.
Validation and process verification: IQ/OQ/PQ in cleanroom injection moulding
Cleanroom production for medical technology and pharma requires validated processes. The three-stage qualification is standard practice: the Installation Qualification (IQ) documents that the mould and equipment are installed correctly and according to specification. The Operational Qualification (OQ) demonstrates that the process runs stably within defined parameter limits. The Performance Qualification (PQ) proves that parts conforming to specification are produced consistently under real production conditions.
Servo-electric mould drives support this verification structurally: position, speed, torque and motor temperature are available digitally as process parameters, parameter sets can be stored reproducibly and deviations documented. What would have to be laboriously retrofitted on hydraulic drives via additional pressure and flow measurement is delivered by the servo controller as an inherent part of the system – a robust basis for OQ and PQ documentation in line with GMP requirements.
Energy consumption: servo-electric vs. hydraulics vs. pneumatics
Energy efficiency is doubly relevant in the cleanroom: every watt of power loss becomes heat that the cleanroom air conditioning has to remove again. Servo-electric drives consume around 75% less energy than hydraulic systems (factor 4) and around 90% less than pneumatic systems (factor 10).
The reason lies in the directness of the servo motors: they convert electrical energy directly into a rotary movement and essentially only draw energy during the movement. In hydraulic drives, by contrast, an electric motor drives a pump that has to maintain the oil pressure permanently – in pneumatic systems, line losses additionally have to be compensated for constantly.
Operating data from the servo controller enables process optimisation and preventive maintenance
The investment in servo-driven mould technology pays off in the long term in terms of control and transparency: the servo controllers record all relevant operating parameters, enabling not only targeted control of the movements but also long-term process optimisation and preventive, condition-based maintenance.
The cleanroom process thus remains documentable and plannable over the entire life cycle of the injection mould.
FAQ – Cleanroom injection moulding
Servo-electric core-pull units and unscrewing units operate free of hydraulic oil. There is no hydraulic fluid that could escape and contaminate components or the cleanroom environment. The movement is clean, defined and repeatable – an important advantage when medical or pharmaceutical plastic parts are produced in the mould.